




PA66 Injection Molded Parts
PA66 is also known as nylon 66, commonly known as nylon double 6; English name: Polyamide 66, abbreviation nylon 66. Nylon-66; Nylon 66 resin; Polyamide-66; PA66 injection molded parts Processable injection molding material types: polyethylene (PE), polypropylene (PP), nylon (PA, PA6, PA66), polyoxymethylene (POM), ABS, polyurethane (TPU), polyphenylene sulfide ( PPS), polycarbonate (PC), polyether ether ketone (PEEK), etc.
PA66 is also known as nylon 66, commonly known as nylon double 6; English name: Polyamide 66, abbreviation nylon 66. Nylon-66; Nylon 66 resin; Polyamide-66; PA66 injection molded parts Processable injection molding material types: polyethylene (PE), polypropylene (PP), nylon (PA, PA6, PA66), polyoxymethylene (POM), ABS, polyurethane (TPU), polyphenylene sulfide ( PPS), polycarbonate (PC), polyether ether ketone (PEEK), etc.
Product Description
1. Implementation standards: the company strictly implements ISO9001, ISO14001, IATF16949, VDA6.3 certification, and products have passed ROHS, FDA EU certification, etc.
2. Product material standards: ISO, GB, ASTM, SAE, EN, DIN, BS, AMS, JIS, ASME, DMS, TOCT, GB
3. Main processes: plastic injection molding, metal insert injection molding, investment casting, die-casting aluminum
4. Available materials for injection molding:
Processable nylon products, plastic products, ABS series; injection molding material types: polyethylene (PE), polypropylene (PP), nylon (PA, PA6, PA66), polyoxymethylene (POM), ABS, polyurethane (TPU), poly Phenyl sulfide (PPS), polycarbonate (PC), polyether ether ketone (PEEK) and 3D printing can be customized according to customer requirements.
Product Feature
PA66 plastic has a higher melting point in polyamide materials. It is a semi-crystalline-crystalline material. PA66 injection molded parts maintain strong strength and stiffness even at higher temperatures. PA66 plastic remains hygroscopic after molding, the extent of which depends primarily on material composition, wall thickness, and environmental conditions. In product design, the effect of hygroscopicity on geometric stability must be considered. In order to improve the mechanical properties of PA66, various modifiers are often added. Glass is the most common additive, and sometimes synthetic rubber is added to improve impact resistance. PA66 plastic is less viscous and therefore flows well (but not as good as PA6). This property can be used to process very thin components. Its viscosity is sensitive to temperature changes. The shrinkage rate of PA66 is between 1% and 2%. Adding glass fiber additives can reduce the shrinkage rate to 0.2% to 1%. The difference in shrinkage in the flow direction and the direction perpendicular to the flow direction is larger. The melting point of PA66 plastic thermal properties is the temperature when the crystal melts. For the crystalline polymer PA66 plastic, it shows a clear melting point. According to the test method used, the melting point fluctuates in the range of 259~267℃. The melting point of PA66 plastic, usually measured by differential thermal analysis, is 264°C. If the temperature at which the volume expansion coefficient shows a maximum value is regarded as the melting point, the melting point temperature of nylon-66 ranges from 246 to 263°C. Close to the theoretical melting temperature of 259 °C. Injection molding characteristics of PA66 plastic drying treatment: If the material is sealed before processing, then drying is not necessary. However, if the storage container is opened, drying in hot air at 85°C is recommended. If the humidity is greater than 0.2%, vacuum drying at 105°C for 12 hours is required.
Melting temperature: 260~290℃. The product of glass additive is 275~280℃. Melting temperatures above 300°C should be avoided.
Mold temperature: 80℃ is recommended. Mold temperature will affect crystallinity, and crystallinity will affect the physical properties of the product. For thin-walled plastic parts, if a mold temperature lower than 40C is used, the crystallinity of the plastic parts will change with time. In order to maintain the geometric stability of the plastic parts, annealing treatment is required.
Injection pressure: usually 750~1250bar, depending on material and product design.
Injection speed: high speed (slightly lower for reinforced materials).
Runners and gates: Due to the short solidification time of PA66, the location of the gate is very important. The gate diameter should not be less than 0.5*t (here t is the thickness of the plastic part). If a hot runner is used, the gate size should be smaller than with conventional runners, as the hot runner can help prevent premature solidification of the material. If a submerged gate is used, the minimum diameter of the gate should be 0.75mm. PA66 plastic application PA66 is the highest mechanical strength and the most widely used variety in the PA series. Because of its high crystallinity, its rigidity and heat resistance are high. High temperature electrical socket parts, electrical parts, gears, bearings, rollers, Spring Brackets, Pulleys, Bolts, Impellers, Fan Blades, Propellers, High Pressure Gaskets, Valve Seats, Oil Pipes, Oil Storage Containers, Ropes, Cable Ties, Transmission Belts, Grinding Wheel Adhesives, Battery Boxes, Insulated Electrical Parts, Wire Cores , threading, etc.
Model
DuPont USA
101F, 101L, 1032L, 103FHS, 103HSL, 10B, 10B40, 11C40-BK, 122L, 135F, 13T1-BK, 151L-NC010, 153HSL-NC010, 3426, 40A, 408HS, 450, 45HSB-NC, 51G35HSL-NC010, 5514,70G13HS1-L,70G13L,70G13SH1L-BK,70G20HSL,70G25HSL,70G30HSLR,70G30L,70G33HS1-L,70G33HS1L-BK,70G33HS1L-NC,70G33L,70G35HSL,70G43L,70K20HSL,71G13L,72G13HS1L,72G33L,72G33HS1L,73G30HSL, 73G30L,73M30,73GM30HSL,74G33L,8018,8018HS,DMX61G15H,DMX65G15AH,DMX65G30AH,DMXST601AH,FE13050,FE15004,FE15033,FE5313-BK,FE5382,FR10,FR15,FR50,FR60,FR52G15BL,FR52G20LX,FR52G30,FR52G30BL,FR52G30LX, FR52G35BL, FR52G45BL, FR53G50HSLR, FR70M30V0, HTN51G15HSL, HTN51G35HSL, HTN52G30NH, ST901L, ST801, ST8018, ST-801HS, ST801NC, ST811HS, ST901HSIL, WRF51G30BL, EFE7374
Asahi Kasei Japan
1300G, 1402S, 14G33, 90G60, 93G33, CR103, FG171, TR161, WG143, 54G33, 91G60, FG172X31, FR250, 1300S, CR301, FR200, FR370, LC020, 1300GT, 13G15, FG172
Ube, Japan
1015GC6, 2015SE50-BK, 2015SV, 2020GC3-NC, 2020GU950, 3020GX6, 3332
Japan's Mitsubishi
3010SR, 3010GN15, 3010N, 3021GH-20, 3021GH-30
BASF, Germany
A3EG6, A3WG6, A3L, A3Z, 8233G, 1403-2, 8231GHS, A3EG3, A3W, A3EG7, A3HG6, A3K, A3W2G5, A3W2G6, A3W2G7, A3WG10, A3WG7
Toray Japan
CM2402, CM3004G25, CM3016-G25, CM1011G45, CM1014, CM1014-V0, CM3001G30, CM3001G33, CM3004, CM3006, CM6021M, HF3074G30, UTN320, E3500, LTP1146S, 2015SV, 2020
Solutia
21SPC, 21X-NC, 220HSP, 22C, 22HSP, 41H, 50BWFS, 909, EC0315, M344, R513, R513H, R530H, R533, 41SP, GW350, Q395, RN5800, 52HSP, 53HSP, 55HSP
Post Injection Molding Process
1. Processing equipment: CNC, WEDM, lathe, milling machine, drilling machine, grinder, etc.;
2. Surface treatment: For some products that require subsequent processing, we can provide surface treatment services to achieve the special purpose of customers. At present, we can provide degreasing, polishing, electroplating (gold, silver, nickel, tin, galvanized, etc.), anodizing, electrophoresis and other surface treatment services for precision parts.

Moulds and Inspection Fixtures
1. Mold service life: usually semi-permanent. (except for lost foam)
2. Mold delivery time: 10-25 days, (according to product structure and product size).
3. Tooling and mold maintenance: Zhongwei is responsible for precision parts.
Quality Control
1. Quality control: the defective rate is less than 0.1%.
2. Samples and trial run will be 100% inspected during production and before shipment, sample inspection for mass production according to ISDO standards or customer requirements
3. Testing equipment: automated visual inspection equipment can carry out 100% inspection of products, spectrum analyzer, golden elephant analyzer, three-coordinate measuring machine, hardness testing equipment, tensile testing machine.
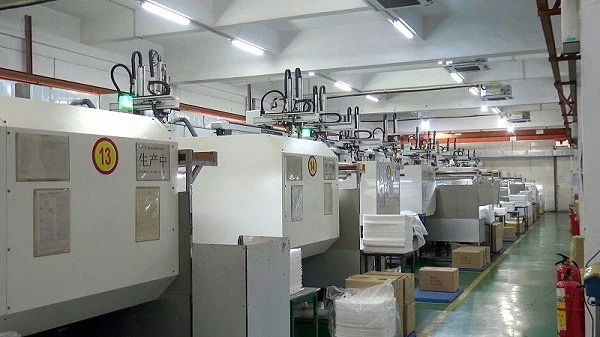
Application
1. Automobile manufacturing:
PA66 injection molded parts are used to make fuel screens, fuel filters, canisters, catchers, oil reservoirs, engine cylinder covers, radiator water cylinders, balance rotary shaft gears. It can also be used in automotive electrical accessories, terminals, etc. In addition, it can also be used as a drive, a control part, and the like.
2. Electrical and electronic industry:
It can be used to manufacture rice cookers, electric vacuum cleaners, high-frequency electronic food heaters, binding posts, switches and resistors for electrical products.
3. Medical equipment and precision instruments:
It is used for medical transfusion vessels, blood drawers, infusion sets, etc. PA monofilament can be used for surgical sutures, wigs, etc.; in addition, digital rotary disks, binding posts, transmission gears of electronic typewriters, belt filters of printing presses, etc.
4. Other aspects:
It is used to make disposable lighter bodies, alkaline dry battery liners, motorcycle drivers' helmets, office machine shells, corner wheels, seats and backrests of office chairs, skates, fishing lines, etc. PA film has excellent gas barrier properties, and It has good oil resistance, low temperature impact resistance and penetration resistance, and can be used for the packaging of frozen food such as meat and ham. Polyamide can also be used in rods and sheets, as well as gears or other transmissions.


Send Inquiry
