




SKD1 Lost Wax Investment Casting
The production process of austenitic stainless steel has good performance, especially chromium-nickel austenitic stainless steel. Conventional means of producing special steel can be used to smoothly produce plates, tubes, strips, wires, bars, forgings, and castings of various commonly used specifications.
Product Introduction
|
SKD1 lost wax investment casting |
|||||||
|
Item |
Material |
Production Process |
Sintering Temperature |
Mold |
Custom |
||
|
SKD1 lost wax investment casting |
SKD1 |
Molten mold casting |
1380℃ |
To be customized |
Yes |
||
|
Chemical composition |
C:≤0.03 Si:≤1.00 Mn:≤2.00 P:≤0.045 S:≤0.015 Cr:17.00~19.50 Mo:— Ni:8.00~10.50 N:≤0.11 |
||||||
|
Available Materials |
Carbon steel, alloy steel, aluminum alloy, low -carbon stainless steel, titanium alloy (TI, TC4), copper alloy, high temperature alloy (718, 713) |
||||||
|
Smoothness |
Dimensional accuracy |
Product density |
Appearance treatment |
Appropriate weight |
|||
|
Roughness 1~5μm |
(±0.1%~±0.5%) |
7.3-7.6g/CM³ |
According to customer requirements |
0.03g~400g) |
|||
Production Process
German standard (EN) X2CrNi18-9 stainless steel, executive standard: DIN 17440-1979,
Belongs to austenitic stainless steel,
The production process of austenitic stainless steel has good performance, especially chromium-nickel austenitic stainless steel. Conventional means of producing special steel can be used to smoothly produce plates, tubes, strips, wires, bars, forgings, and castings of various commonly used specifications.
Austenitic stainless steels can also be used to produce castings. In order to improve the fluidity of molten steel and improve casting performance, the alloy composition of cast steel should be adjusted: increase the silicon content, relax the range of chromium and nickel content, and increase the upper limit of the impurity element sulfur.
X2CrNi18-9 stainless steel, German DIN standard stainless steel. Corresponding to 022Cr19Ni10, the corresponding number we are more familiar with is 304L. Compared with ordinary 304, 304L has lower carbon content and there is not much difference in mechanical properties. Mainly used in welding, because the carbon content is relatively low, which can increase the ability to resist intergranular corrosion. (The carbon content of ordinary 304 is min. 0.15%, and that of 304L is min. 0.030%. 304L should be softer).
Brand: X2CrNi18-9
Standard: DIN 17400
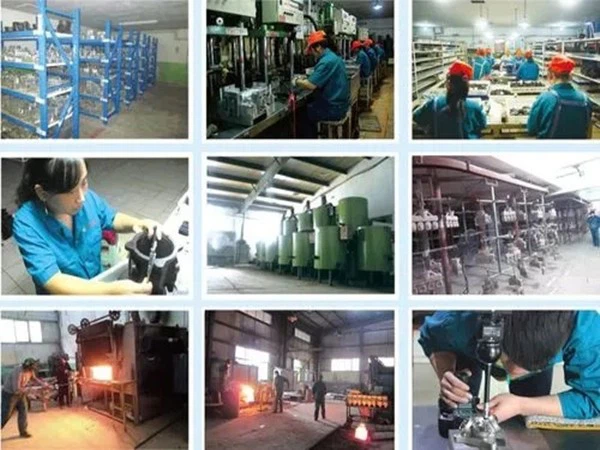
The so-called investment casting process simply means using fusible materials (such as wax or plastic) to make a fusible model (referred to as investment mold or model), coating it with several layers of special refractory paint, and drying and hardening it. After forming an overall mold shell, use steam or hot water to melt the model from the mold shell, then place the mold shell in a sandbox, fill it with dry sand molding around it, and finally put the mold into a roasting furnace and pass through a high-temperature Baking (if a high-strength mold is used, the molded shell can be directly baked without molding). After the mold or shell is baked, molten metal is poured into it to obtain a casting.
The dimensional accuracy of investment castings is relatively high, generally up to CT4-6 (CT10~13 for sand casting, CT5~7 for die casting). Of course, due to the complexity of the investment casting process, there are many factors that affect the dimensional accuracy of castings, such as mold The shrinkage of the material, the deformation of the investment mold, the linear volume changes of the mold shell during the heating and cooling process, the shrinkage rate of the alloy and the deformation of the casting during the solidification process, etc. Therefore, although the dimensional accuracy of ordinary investment castings is high, its consistency still needs to be improved (the dimensional consistency of castings using medium and high-temperature wax materials needs to be much improved).
When pressing the investment mold, a mold with a high surface finish of the cavity is used, so the surface finish of the investment mold is also relatively high. In addition, the mold shell is made of a refractory coating made of high-temperature-resistant special binders and refractory materials and is hung on the investment mold. The inner surface of the mold cavity that is in direct contact with the molten metal has a high smoothness. Therefore, the surface finish of SKD1 lost wax investment casting is higher than that of ordinary castings, generally reaching Ra.1.6~3.2μm.
Detection Systems

Copper Silica Sol Investment Casting


Send Inquiry
