



44-12 Bicycle Tire Anti-skid Spikes Metal Injection Molding Parts
Pursue excellence, continue to innovate, and provide customers with satisfactory high-quality products and excellent services

A method for preparing a high specific gravity tungsten-based alloy, comprising the following steps:
(1) Mixing ingredients: weigh 7.31 kg of tungsten powder, 1.88 kg of nickel powder, and 0.81 kg of iron powder to obtain a mixture A;
(2) Dry grinding: dry grind the mixture A at a speed of 30 rpm for 6 hours and mix evenly;
(3) Mixing and granulation: stir the mixture A treated in step (2) at a speed of 15 rpm under nitrogen protection, preheat at 200°C for 25 minutes; heat up and add 107.2 g of plastic auxiliary materials (HDPE: EVA: wax: SA (weight ratio is 7:2:2:1) and 785g of polyoxymethylene resin (POM), then heated to 230℃, kept warm for 10min, after POM melted, put down the pressing cover plate for internal mixing, and start cooling at the same time. After cooling to 200℃, continue internal mixing for 15min until the surface of the material is uniform and smooth, and then cool to 180℃ and extrude through the screw and cut into pellets;
(4) Injection molding: After making the mold according to the product size and material shrinkage requirements, install the mold into the injection molding machine, put the pellets prepared in step (3) into the injection molding machine hopper, and inject the molten material into the mold cavity through the barrel to form it; the specific injection molding parameters include: the barrel temperature is set at 160-200℃, the injection pressure is 80-130Bar, and the injection speed is 35%-70%;
(5) Degreasing: Catalytic degreasing is carried out in three steps , the first step: flush the furnace cavity with nitrogen to remove the air in the furnace cavity; the second step, atomize pure nitric acid gas and pass it into the furnace cavity to make it react chemically with the polyoxymethylene resin in the product, decompose more than 80% of the polyoxymethylene resin in the MIM injection molding blank into formaldehyde gas and discharge it; the third step: flush the furnace cavity with nitrogen to flush the residual acid mist in the furnace cavity;
(6) Sintering: vacuum sintering in a graphite furnace, sintering is divided into three stages, the first stage, below 800℃, the polyoxymethylene resin and plastic auxiliary materials remaining in the product blank after degreasing are gasified and discharged at high temperature; the second stage, at 800-1410℃, the nickel metal and iron metal in the blank form a liquid phase at high temperature, and the tungsten metal is integrated into it and sintered into shape; the third stage, the temperature in the furnace is cooled to below 70℃ and the product is taken out; the sintering time is 23-26h.
The performance parameters of the high-density tungsten-based alloy obtained by the above preparation method are as follows:
| Product density | 14±0.1g/cm3 |
| Product hardness | HRC25±5. |
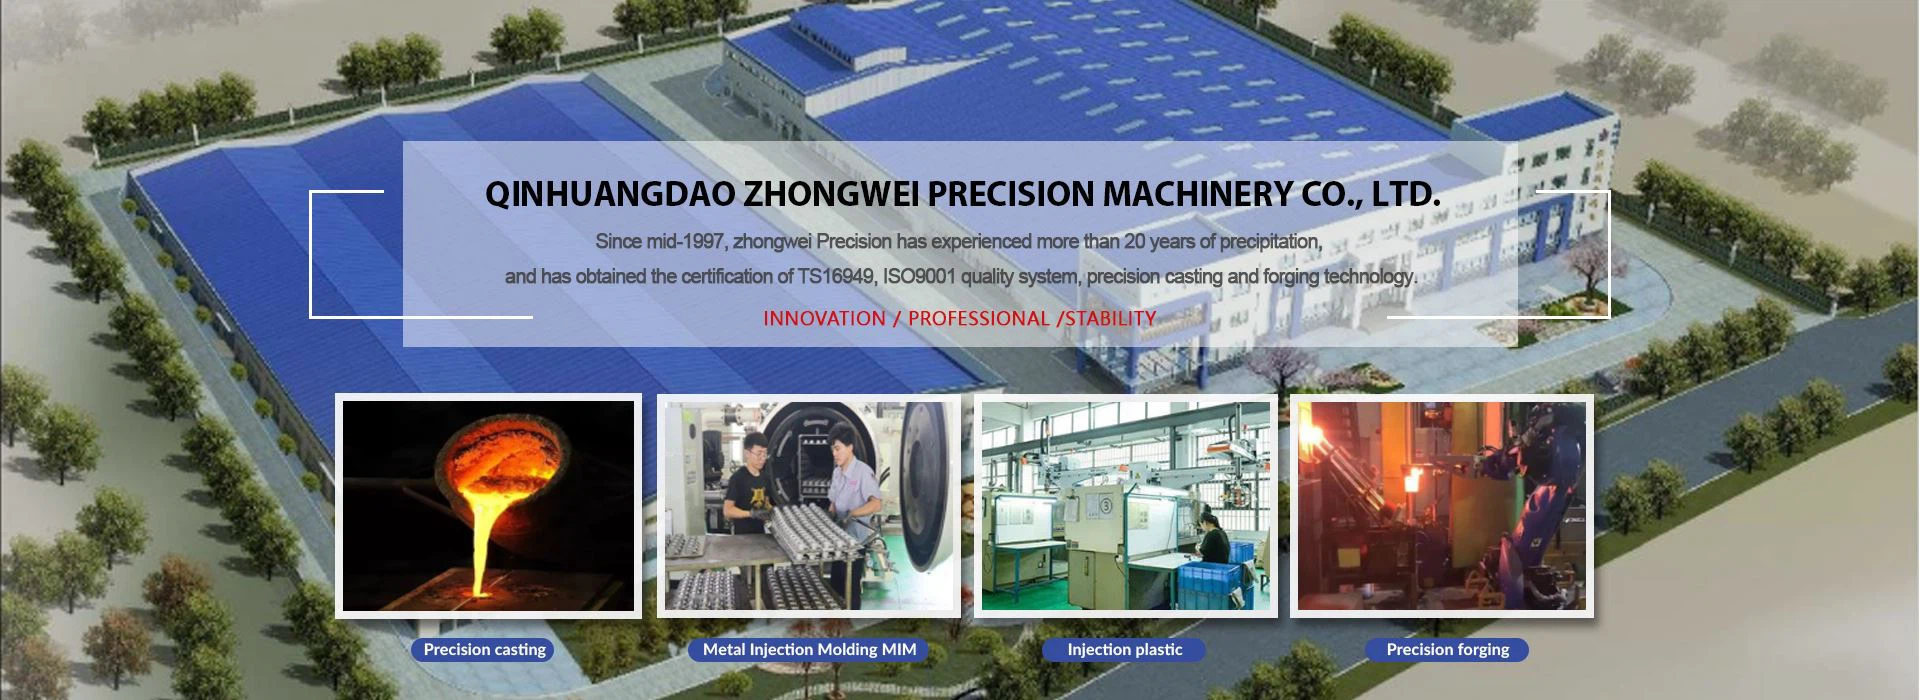
Qinhuangdao Zhongwei Precision Machinery Co., Ltd. is a technology-based enterprise integrating high-tech technologies such as powder metallurgy, metal injection, carbide, and transmission gearboxes. In the past 20 years, the company has built a modern factory with various advanced manufacturing equipment and professional testing equipment. It has also cooperated with more than a dozen Fortune 500 companies and achieved outstanding results in the industry while catering to the global market. 2003--Passed ISO9001:200 0 quality certification system 2011--Passed ISO/TS16949.2009 automotive parts supplier quality certification system 2017--IATF16949:2016 automotive parts supplier quality certification system 2019 Passed ISO14001 environmental management system certification Supporting industries: automobiles, motorcycles, power tools, household appliances, communication equipment (mobile phones), smart wearables, mold carbide materials and pressure-resistant and wear-resistant high-strength alloys, garden tools and medical equipment and other applicable industries. Product features of our company: high strength, high precision, high cost performance, research and development and customization of special-shaped parts, supporting structural parts, and mass production Our business purpose: pursue excellence, continue to innovate, and provide customers with satisfactory high-quality products and excellent services. Our slogan: Technological innovation quality, Zhongwei keeps pace with the times



Send Inquiry
