




Lost Foam Casting Ductile Iron
Lost Foam Casting Ductile Iron process precautions and ductile iron lost foam casting requirements. At present, my country's lost foam process has developed rapidly, but there are still many manufacturers who have not been exposed to the lost foam process before.
Qinhuangdao Zhongwei Precision Machinery Co., Ltd. has accumulated rich clinical experience in the production process of EPC lost foam for more than ten years, and has dealt with difficult problems on site for many manufacturers and developed dozens of complex thin-walled parts. The varieties developed by the factory include gearbox housing, air conditioner compressor body, high-speed impeller pump body, oil pump body, pump body and valve body, which have been well received by customers. The lost foam coating developed by the factory has been favored by customers in many manufacturers. The factory has built a new lost foam production line with an annual output of 6000T to 10000T. We hope that people of insight will come to the factory to negotiate with Lost Foam Casting Ductile Iron and create a brilliant future.
Product Description
Basic information about Lost Foam Casting Ductile Iron
1.Implementation standards: The company strictly implements ISO9001 & TS 16949 certification.
2. Product material standards: ISO, GB, ASTM, SAE, ISO, EN, DIN, JIS, BS
3. Main processes: sand casting, silica sol investment casting, water glass investment casting,shell casting,deburring, sand blasting, machining, heat treatment, leak testing, surface treatment, etc.
4. Available materials:
Tin bronze, silicon bronze, aluminum bronze, brass, copper, titanium alloy, high manganese steel, high chromium steel, high nickel steel, carbon steel, alloy steel, stainless steel, gray iron, cast iron, cast steel, cast aluminum, etc. Customized according to customer requirements.
Casting Process
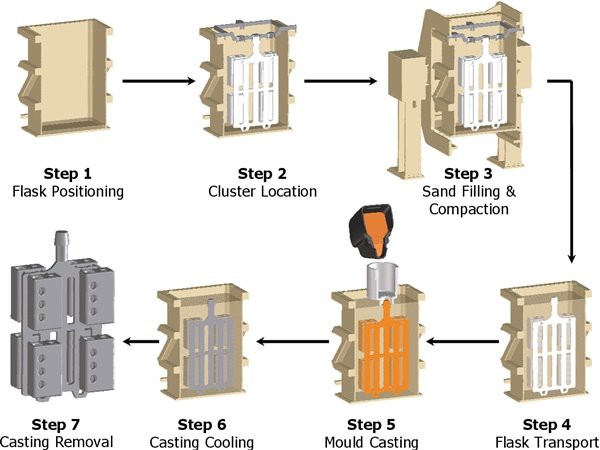
Lost Foam Casting Ductile Iron process precautions and ductile iron lost foam casting requirements. At present, my country's lost foam process has developed rapidly, but there are still many manufacturers who have not been exposed to the lost foam process before. They start production and often visit many companies. Afterwards, I thought it was very simple, and I thought I would know it. The lost foam casting process can make many types of products, with the characteristics of precision casting, and can also be produced on a large scale. , today is to introduce the precautions when pouring ductile iron.
1.The first is to heat up the furnace to 1650-1680 degrees to ensure carbon silicon.
2. Weigh the alloy into the casting ladle, and then add ferrosilicon to cover the layer at 30/40mm.
3. Pour one-third of the original molten iron first, and then add two-thirds of the molten iron after the reaction is completed.
4. While introducing the pouring ladle, add the corresponding amount of ferrosilicon for secondary inoculation.
5. The slag time and the driving time should be shortened to the greatest extent, so that the molten iron can be rushed into the box quickly.
6. The negative pressure should be fixed at a constant temperature. After pouring, the pressure should be maintained according to the casting conditions, and then out of the box.
It should be noted that the temperature required for different castings is different, and the pressure holding time and the time out of the box are also different. Reasonable configuration according to the castings can achieve the best results. The above is a brief introduction to the lost foam casting ductile iron process of Zhongwei Precision.
Analysis Of Quality Problems And Reasons For Improvement
Problems found by Lost Foam Casting Ductile Iron:
1. Apparent trachoma,
The main reasons are: ① The slag liquid formed after the spheroidization of molten iron is not completely removed. After pouring, it enters the cavity and forms slag holes on the surface of the casting. ②The exhaust of individual products is not smooth, forming pores.
Corrective measures: ① After the molten iron is spheroidized, the slag is thoroughly cleaned, and the lining of the ladle is regularly replaced to prevent the occurrence of slag holes. ②Put the vent holes in the easy-to-collect part of the cavity to prevent the generation of stomata. ③After machining, before the product leaves the factory, strictly check the inspection to prevent defective products from leaving the factory.
2. The internal shrinkage cavity causes oil leakage during the pressure test.
The main reason is that the pouring temperature is too high, and the slow pouring speed leads to shrinkage cavities when the internal shrinkage occurs.
Corrective measures: ① For the pouring temperature and pouring speed, re-determine the process parameters, and monitor and measure to prevent the occurrence of internal sink holes. ② Before the process parameters are verified and confirmed, the machined products shall be tested for flaws one by one, and qualified products shall be selected for delivery. Perform flaw detection on all products in stock, and reject unqualified products.
3. The product material is hard and difficult to process.
The main reason is: poor product breeding causes component segregation and forms hard spots.
Corrective measures: re-verify the inoculation process, determine the amount and method of adding inoculants, and prevent the segregation of the slugs from causing the problem of material hardness.
Post Casting Process
1. Heat treatment: annealing, carbonization, tempering, quenching, normalizing, surface tempering
2. Processing equipment: CNC, WEDM, lathe, milling machine, drilling machine, grinder, etc.;
3. Surface treatment: powder spraying, chrome plating, painting, sandblasting, nickel plating, galvanizing, blackening, polishing, bluing, etc.
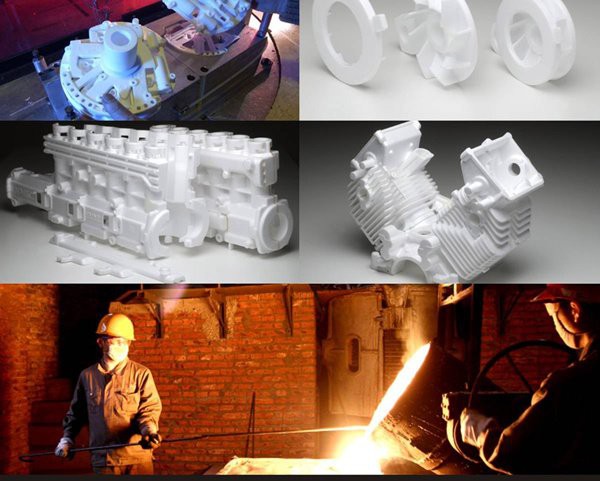
Moulds and Inspection Fixtures
1. Mold service life: usually semi-permanent. (except for lost foam)
2. Mold delivery time: 10-25 days, (according to product structure and product size).
3. Tooling and mold maintenance: Zhongwei is responsible for precision parts.
Quality Control
1. Quality control: the defective rate is less than 0.1%.
2. Samples and trial run will be 100% inspected during production and before shipment, sample inspection for mass production according to ISDO standards or customer requirements
3. Testing equipment: flaw detection, spectrum analyzer, golden image analyzer, three-coordinate measuring machine, hardness testing equipment, tensile testing machine;
4. Provide after-sales service.
5. The quality can be traced back.


Send Inquiry
