




Forklift Shed Bollard Lost Wax Investment Casting
Since the forklift may encounter the goods on the forks or surrounding objects falling from high places during the operations of dismantling, stacking, and transferring goods. In order to ensure the safety of the operators, a roof guard is installed above the operators.
Product Introduction
|
Forklift shed bollard lost wax investment casting |
|||||||
|
Item |
Material |
Production Process |
Sintering Temperature |
Mold |
Custom |
||
|
Forklift shed bollard |
Investment casting |
1680℃ |
To be customized |
Yes |
|||
|
Available Materials |
Carbon Steel, Alloy Steel, Aluminum Alloy, Low Carbon Stainless Steel, Titanium Alloy (Ti, TC4), Copper Alloy, Superalloy (718, 713) |
||||||
|
Smoothness |
Dimensional accuracy |
Product density |
Appearance treatment |
Appropriate weight |
|||
|
Roughness Ra3.2-6.3μm |
Ct4-ct8 |
7.8/CM³ |
According to customer requirements |
100g~25kg |
|||
Forklift Overhead Guard Roof
Since the forklift may encounter the goods on the forks or surrounding objects falling from high places during the operations of dismantling, stacking, and transferring goods. In order to ensure the safety of the operators, a roof guard is installed above the operators. It is very necessary.
The roof guard of a traditional forklift is parallel to the ground, and the impact force is concentrated, resulting in a decrease in its ability to resist falling impacts. And because we often encounter special weather conditions in the process of using traditional forklifts for operations and teaching, such as rain, snowfall, high temperature, etc. The traditional forklift roof guard roof does not consider the corresponding design, resulting in certain limitations in the use of this type of forklift. Therefore, a new type of forklift overhead guard roof structure is proposed to solve the above-mentioned problems.
The purpose of this utility model is to propose a new type of forklift roof guard in order to solve the shortcomings existing in the prior art.
In order to achieve the above purpose, the present utility model adopts the following technical measures:
A new type of forklift overhead guard roof includes a support frame. The inclined ceiling is set on the support frame through uprights. A grid is provided on the higher side of the inclined ceiling. A placement slot is provided on the lower side of the inclined ceiling. The upper side of the placement slot is covered with a grid. There is a slot cover, a tarpaulin outlet is provided on the slot cover, a hook is provided on the support frame below the higher side of the inclined ceiling, and an awning telescopic mechanism is provided in the placement slot.
The awning telescopic mechanism includes two stators respectively arranged at both ends of the placement slot and a rotor arranged between the two stators. A through-connecting column is provided in the center of the stator, and rotor end perforations are respectively provided on both end surfaces of the rotor. Rotor convex rings are also respectively provided on the rotor. The threaded end of the rotor limiting bolt passes through the through-connecting column and the rotor end surface hole in sequence and is connected to the limiting nut. The flat nest-type spring is sleeved on the through-connecting column. One end of the flat nest-type spring is connected to the through-connecting column. The connecting post is connected and the other end is connected to the rotor convex ring. The tarpaulin is rolled on the rotor. The inner end of the tarpaulin is connected to the tarpaulin connection port on the rotor. The outer end of the tarpaulin passes through the tarpaulin outlet and is provided with a hook. Adaptable hanging head.
As mentioned above, the stator is provided with a stator convex ring that is buckled outside the rotor convex ring. The stator convex ring is provided with a stator positioning hole. The slot cover is provided with a slot cover positioning hole. The pins penetrate the slot cover positioning holes and the stator in turn. Positioning holes.
Compared with the existing technology, this utility model has the following beneficial effects:
1. The sloping ceiling has an inclined design. When a falling object impacts the support frame, there is first line contact and then gradually becomes surface contact. The load acts smoothly, which helps to reduce the impact force. The inclined design increases the elevation angle and also helps to increase the impact force. Driver's forward view;
2. The design of the support frame and the upper and lower layers of the inclined roof is conducive to increasing the distance between the driver's seat and the inclined roof, thereby expanding the driver's living space after the inclined roof is impacted.
3. The design of the awning telescopic mechanism can overcome the normal operation of the forklift in special weather such as rain, snowfall, high temperature, etc.
Investment Casting Process
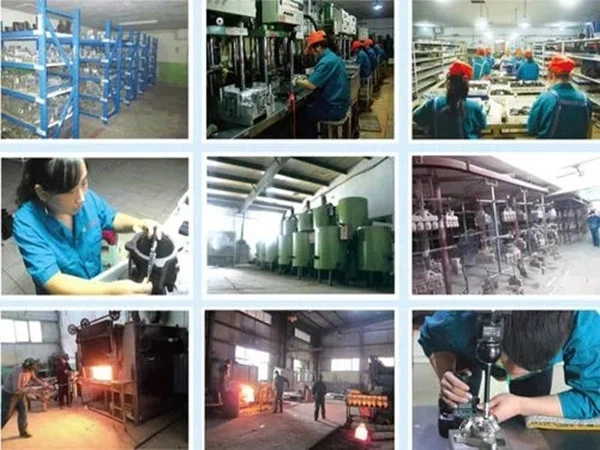
Investment casting, also known as lost wax casting, includes processes such as wax pressing, wax trimming, tree assembly, slurry dipping, wax melting, molten metal casting and post-processing. This is a casting process that has very ancient origins but is still widely used today.
Principles Of Investment Casting Process
The so-called investment casting process is simply a casting process that uses easily meltable materials to make soluble molds, also called investment molds, and uses them to process metal castings.
The material used to make the investment mold can be wax or plastic. After the Forklift shed bollard lost wax investment casting is formed, it needs to be coated with several layers of special refractory paint. After drying and hardening, an integral shell is formed. For the overall mold shell, steam or hot water needs to be used to melt the model from it, and then the mold shell is placed in a sand box and filled with dry sand molding around it. Finally, the casting mold filled with dry sand is placed in a roasting furnace and roasted at high temperature. After roasting, molten metal can be poured into it to obtain a casting.
Operational Flow Of Investment Casting Process
The first step is to take out the wax cylinder from the thermal insulation tank, remove the air mixed in the wax material and the hard wax produced due to long-term exposure, and install the wax cylinder on the double-station hydraulic wax mold injection machine.
In the second step, the mold needs to be placed on the work surface of the injection machine for positioning. All core positions of the mold must be correct. Check whether the wax injection port of the mold is aligned with the wax injection nozzle of the injection machine, and whether the mold opens and closes smoothly.
The third step is to open the mold and spray a thin layer of parting agent on the inner and outer surfaces.
The fourth step is to adjust the cycle time, injection pressure, injection temperature, holding time and cooling time of the injection machine according to the technical requirements. After the cycle is completed, pull out the core and open the mold. Carefully remove the wax mold and place it in cooling water or a storage tray as required.
The fifth step is to remove the remaining mold material from the mold. This process can only be completed with a bamboo knife. Remember not to use metal blades, which can easily cause damage to the mold cavity and parting surface.
The final step is to close the mold and proceed to the next wax pattern pressing.
Detection Systems

Copper Silica Sol Investment Casting



Send Inquiry
