




Forklift Base Lost Wax Investment Casting
In the prior art, when preparing the box base of a forklift, the usual method is to bend the sheet metal twice, and then connect and shape the bent sheet metal through welding to form the box base. The disadvantage is that it increases the amount of wood used and the process of making the box, and takes up a certain amount of man-hours for making the box, thereby increasing the cost of making the box.
Product Introduction
|
Forklift Base Lost Wax Investment Casting |
|||||||
|
Item |
Material |
Production Process |
Sintering Temperature |
Mold |
Custom |
||
|
Forklift Base |
Investment casting |
1680℃ |
To be customized |
Yes |
|||
|
Available Materials |
Carbon Steel, Alloy Steel, Aluminum Alloy, Low Carbon Stainless Steel, Titanium Alloy (Ti, TC4), Copper Alloy, Superalloy (718, 713) |
||||||
|
Smoothness |
Dimensional accuracy |
Product density |
Appearance treatment |
Appropriate weight |
|||
|
Roughness Ra3.2-6.3μm |
Ct4-ct8 |
7.8/CM³ |
According to customer requirements |
100g~25kg |
|||
In the prior art, when preparing the box base of a forklift, the usual method is to bend the sheet metal twice, and then connect and shape the bent sheet metal through welding to form the box base. The disadvantage is that it increases the amount of wood used and the process of making the box, and takes up a certain amount of man-hours for making the box, thereby increasing the cost of making the box. The specific performance is as follows: when the existing base is made, considering its own strength problem, it is impossible to open a forklift hole on the base for box transportation. The transportation of the box is assisted by making a wooden base and placing it on the bottom of the sheet metal base. Box transportation work.
Technical Implementation Elements
The purpose is to provide a base with a forklift slot that is easy to transport and low cost.
The technical solution adopted by the present invention is: a base with a forklift slot, and the base with a forklift slot includes:
2 horizontal frames, the horizontal frames extend in the left and right directions, and the horizontal frames each include a horizontal vertical plate located in a vertical plane, and two inner sides are vertically connected to the upper sides of the corresponding horizontal vertical plates. and transverse reinforcing plates on the lower side and extending horizontally outward. At the same time, the outer edges of the transverse reinforcing plates located on the opposite lower side are vertically bent upward and extended to form transverse ribs. The middle part of the transverse vertical plate is provided with a 2 square holes for forklift slots;
There are 4 middle frames, each of which includes a middle vertical plate located in a vertical plane, 2 middle reinforcing plates whose sides are vertically connected to the upper and lower sides of the corresponding middle vertical plate, and 2 Each inner side is vertically connected to the middle top plate on the front side and rear side of the corresponding middle vertical plate respectively;
2 longitudinal frames, each of which includes 1 vertical vertical plate located in a vertical plane, 2 inner sides vertically connected to the upper and lower sides of the corresponding vertical vertical plate and both facing outwards horizontally The extended longitudinal reinforcing plate and the two inner sides are respectively vertically connected to the front and rear sides of the corresponding longitudinal vertical plate and both extend outward. At the same time, the longitudinal reinforcing plate located on the opposite lower side is The outer edge is vertically bent and extended upward to form a longitudinal rib, and the sides of the side top plates are welded to the sides of the corresponding longitudinal reinforcing plates;
as well as
The two horizontal borders are set parallel, one behind the other;
The middle top plates of the four middle frames are supported on and welded to the inner side of the transverse vertical plates of the corresponding horizontal frames. There is a middle frame on both sides of the square hole of each forklift slot;
The side top plates of the two longitudinal frames are supported on and welded to the left and right ends of the inner sides of the transverse vertical plates of the corresponding transverse frame.
The inner side of the middle vertical plate is flush with the left or right side of the corresponding square hole of the forklift slot.
Compared with the prior art, the present invention has the advantages of convenient transportation and low cost. The three components required for the base with forklift slots of the present invention are connected together by welding. On the premise of ensuring the load-bearing capacity of the base, two holes at the forklift corners are opened on the base. The forklift can transport the box directly through the base. The transportation work of the box body and the box body no longer requires other auxiliary workpieces to complete. At the same time, in order to ensure the load-bearing capacity of the base, during the production of the three parts of the base, a bent reinforcement plate was made on each part to strengthen the sheet metal, which not only facilitates forklifts to lift the box transportation, and can increase the load-bearing load of the base to the weight of the box. In this way, no wood is wasted during preparation, material and labor costs are saved, and it is easy to use.
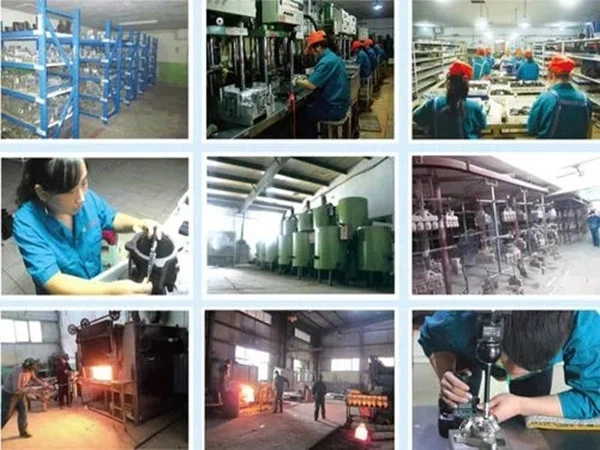
Investment Casting
When using wax to make patterns, investment casting is also known as "lost wax casting". Investment casting usually refers to the casting scheme in which the pattern is made of fusible materials, the shell is made by coating several layers of refractory materials on the surface of the pattern, and then the pattern is melted and discharged out of the shell, so as to obtain a casting model without parting surface, and the casting scheme can be filled with sand and poured after high temperature roasting. Because the pattern is widely made of wax materials, investment casting is often referred to as "lost wax casting". The types of alloys that can be produced by investment casting method include carbon steel, alloy steel, heat-resistant alloy, stainless steel, precision alloy, permanent magnet alloy, bearing alloy, copper alloy, aluminum alloy, titanium alloy and ductile iron.
The shape of investment castings is generally more complex, the minimum diameter of the hole that can be cast on the casting can reach 0.5mm, and the minimum wall thickness of the casting is 0.3mm. In production, some parts that were originally composed of several parts can be designed into integral parts and directly cast by investment casting by changing the structure of the parts, so as to save processing man-hours and the consumption of metal materials, and make the part structure more reasonable. The weight of investment castings is mostly zero to tens of cattle (from a few grams to more than ten kilograms, generally not more than 25 kilograms), and it is more troublesome to produce too heavy castings by investment casting.
The forklift Base Lost Wax Investment Casting process is complex, difficult to control, and expensive to use and consume materials, so it is suitable for producing small parts with complex shapes, high precision requirements, or difficult to perform other machining, such as turbine engine blades.
Detection Systems

Copper Silica Sol Investment Casting



Send Inquiry
